RayForm Technical Guide · Model Resin Profiles
Dental Resin Print Settings for Phrozen and Anycubic
Getting consistent results from dental resin 3D printing requires more than choosing a resin and entering a single exposure value. Printer model, light output, layer height, resin formulation, orientation and post-processing conditions can all affect print quality, dimensional accuracy and build reliability. Even two printers from the same brand may require different settings for the same material.
For dental labs and 3D printing users working with Phrozen or Anycubic printers, starting with a verified printer–resin profile can reduce unnecessary trial and error. In this guide, we look at selected RayForm dental resin print settings for Phrozen and Anycubic machines, explain how to calibrate exposure parameters, troubleshoot common printing problems, and use the RayForm Parameter Database to establish a practical starting point for your own workflow.
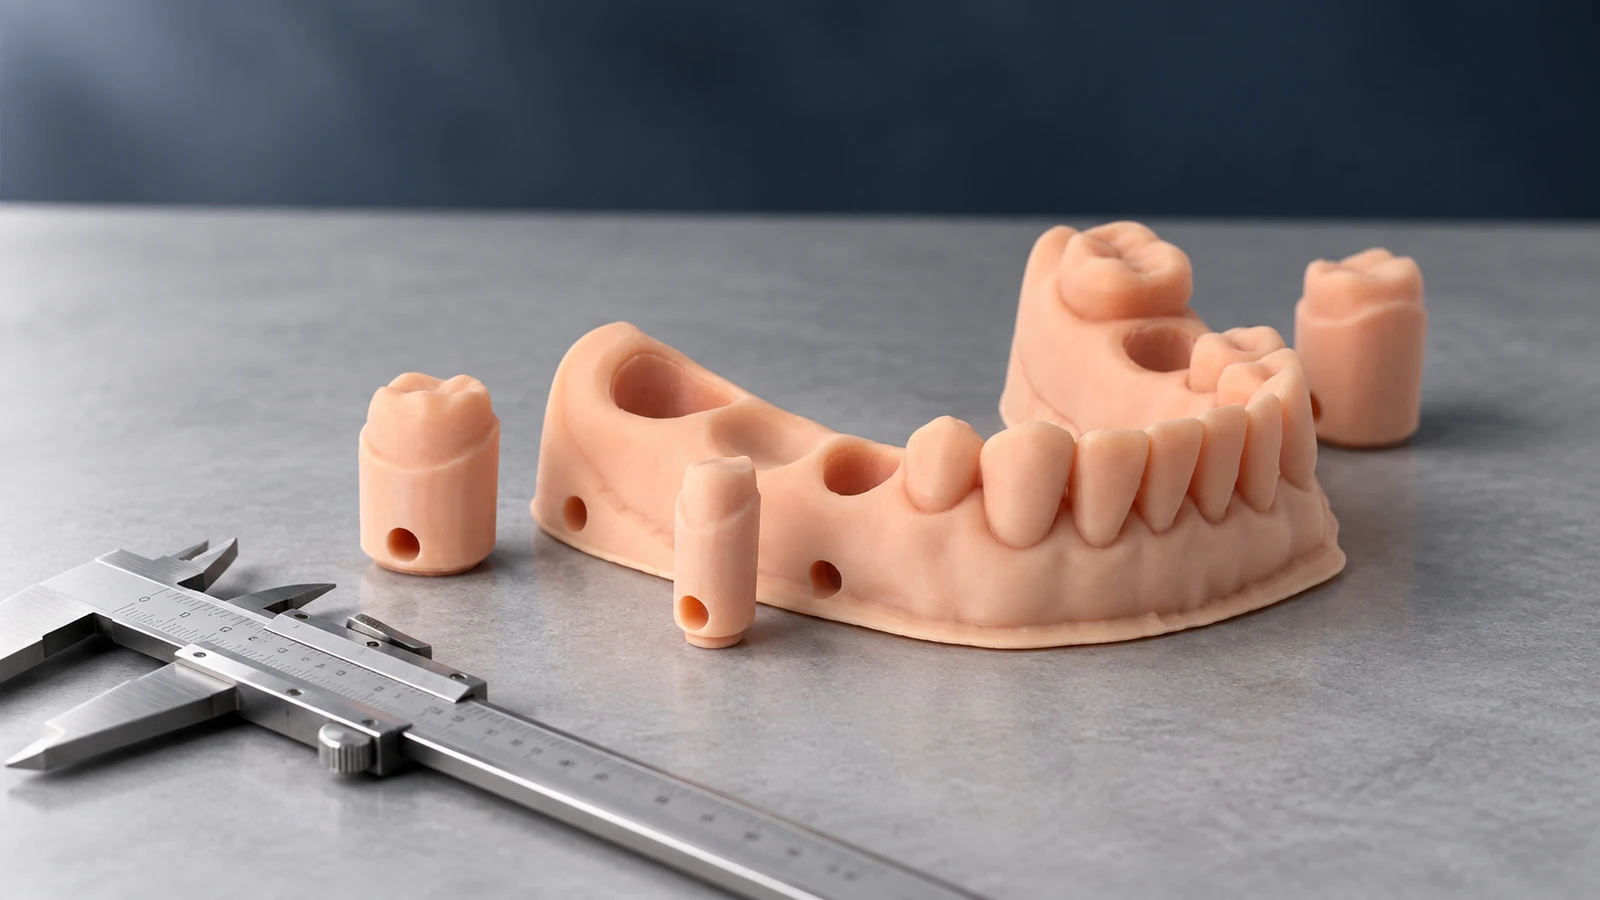
Dental resin print settings: what you need to know
Start with the exact printer, resin and layer height. Use the complete profile as your baseline, check a calibration print, then confirm representative parts after the required post-processing. An exposure value alone does not define a production-ready workflow.
The right dental resin print settings help you reproduce fine details, maintain dimensions and reduce failed builds. However, a profile that works on one printer should not automatically be applied to another—even when both machines use the same resin and layer height.
Printers differ in light delivery, optical systems, separation mechanisms and software controls. Materials also respond differently according to formulation, color and processing conditions. Start with settings for your exact printer–resin combination, then confirm the results on your equipment.
- Printer configuration: light output, optical characteristics, hardware condition and motion control affect the printing process.
- Resin formulation: material version, pigmentation and viscosity influence how a resin prints.
- Layer height: exposure must correspond to the selected layer thickness; changing one can require reassessing the other.
- Preparation and environment: follow the material's mixing, storage and processing-temperature instructions.
- Part setup: orientation, supports and cross-sectional geometry affect release forces and feature reproduction.
Phrozen & Anycubic print settings
The tables below reproduce selected combinations from RayForm’s published parameter database, checked on September 23, 2026. They provide exposure starting points. Use the full corresponding profile for motion, delays and other settings, and confirm the exact resin version before printing. [1]
Phrozen: Sonic Mini 8K S and Mini 4K
For Phrozen, select the full model name rather than relying on the Sonic family name alone. The examples below show separate settings for Sonic Mini 8K S and Sonic Mini 4K.
| Printer model | RayForm resin label | Layer height | Normal exposure | Bottom exposure | Bottom layers |
|---|---|---|---|---|---|
| Sonic Mini 8K S | Water washable | 0.05 mm | 4.5 s | 25 s | 3 |
| Sonic Mini 8K S | Model resin | 0.05 mm | 4.6 s | 25 s | 3 |
| Sonic Mini 4K | Water washable | 0.05 mm | 6.8 s | 38 s | 3 |
| Sonic Mini 4K | Model resin | 0.05 mm | 6.9 s | 38 s | 3 |
On a small screen, scroll the table horizontally to view every setting.
Anycubic: Photon Mono M7 and M7 Pro
Anycubic model suffixes also matter. Select the M7 or M7 Pro entry that matches your machine; do not assume their profiles are interchangeable.
| Printer model | RayForm resin label | Layer height | Normal exposure | Bottom exposure | Bottom layers |
|---|---|---|---|---|---|
| Photon Mono M7 | Water washable | 0.05 mm | 3.2 s | 23 s | 4 |
| Photon Mono M7 | Model resin | 0.05 mm | 3.3 s | 23 s | 4 |
| Photon Mono M7 Pro | Water washable | 0.05 mm | 2.3 s | 16 s | 4 |
| Photon Mono M7 Pro | Model resin | 0.05 mm | 2.4 s | 16 s | 4 |
On a small screen, scroll the table horizontally to view every setting.
Source: RayForm Printer Parameter Database. Resin labels follow the database; confirm the product code and version when matching a bottle. These abbreviated tables do not include the complete printing or post-processing instructions. [1]
How to calibrate dental resin settings
BASE PROFILE → TEST PRINT → INSPECT → ADJUST → CONFIRM
Use a controlled sequence: start with the base profile, print a test, inspect the result, adjust exposure if needed, then confirm and save the final settings. Keep the test geometry and processing conditions consistent so you can identify what each change does.
Manufacturer tools can help with the exposure test: Phrozen documents its XP Finder, and Anycubic explains its Resin Exposure Range Finder. Follow the instructions for your own printer and supported file format. These tests help assess exposure; a dental production workflow still needs checks on the parts you actually intend to print. [3] [4]
Use the base settings
Select the exact printer, resin and layer-height combination. Enter or import the full profile, check units, and complete the printer manufacturer's setup checks. Prepare the resin according to its instructions.
Print a test
Use the supplier's recommended calibration file or a model with measurable features relevant to your work. Record the profile version, resin batch, temperature and build position. Keep orientation and supports unchanged between exposure tests.
Inspect the result
Check plate adhesion, layer integrity, openings, fine details and visible defects. Complete the prescribed post-processing before judging final dimensions. Measure selected features against the design rather than relying only on appearance.
Adjust exposure
First rule out setup, material-preparation and support problems. If the evidence indicates insufficient exposure, test a small increase in normal exposure within the supplier's permitted range. If it indicates overexposure, test a small decrease. Reprint the same test and change one variable at a time. Treat bottom exposure separately when investigating plate adhesion.
Confirm the final settings
Repeat the successful test and evaluate a representative production part. Check relevant build positions and finished dimensions against your acceptance criteria. Save the accepted profile with the printer model, resin version, layer height, date and processing instructions.
Do not apply a fixed exposure adjustment percentage to every resin. If changes fail to improve the result or no adjustment range is provided, send the test results to technical support. Recheck the setup after material changes, significant maintenance or software changes that may affect printing.
Common printing problems & solutions
A visible defect can have more than one cause. Use the table to decide what to inspect before changing the profile; make controlled adjustments within the supported workflow.
Printer guidance also identifies plate setup, temperature, support strength and motion settings as possible contributors to print failures. Check the cause before changing exposure. [5]
| Problem | Possible causes | Adjustment or corrective action |
|---|---|---|
| Parts detach from the build plate. | Incorrect plate setup, contamination, insufficient bottom exposure or unsuitable first-layer conditions. | Clean and check the plate according to the printer instructions. Confirm resin preparation and bottom settings. If inadequate bottom exposure is established, increase it incrementally within the supported range and retest. |
| Layer separation or delamination. | Insufficient normal exposure, excessive separation forces, weak supports or unsuitable processing temperature. | Check temperature, supports and the full motion profile. If underexposure is confirmed, increase normal exposure slightly and repeat the test. Reassess orientation or motion with supplier guidance when release forces are the issue. |
| Fine details are blurred or small openings close. | Overexposure, smoothing settings, limited source geometry or residual resin after cleaning. | Inspect the file and cleaning result first. If overexposure is confirmed, reduce normal exposure slightly and reprint. Review anti-aliasing or smoothing settings separately. |
| Dimensions are inaccurate. | Incorrect profile, exposure-related feature growth, calibration errors or changes during post-processing. | Measure consistent features after the prescribed processing. Check printer calibration and material identity, then adjust the confirmed source of error. Do not use a global scale change to hide inconsistent distortion. |
| Supports print but the part fails. | Inadequate support contacts, unsuitable orientation, high separation loads or insufficient part strength during printing. | Review support placement and orientation. Confirm the material and motion profile before changing exposure. |
| The finished surface remains tacky. | Incomplete cleaning, inadequate drying or incorrect curing conditions. | Check cleaning effectiveness and the specified drying and curing process. Do not assume additional exposure during printing will correct a post-processing problem. |
On a small screen, scroll the table horizontally to view causes and corrective actions.
Using the RayForm Parameter Database
Starting from an identified printer–resin profile can reduce the time spent searching for a workable baseline. The RayForm Parameter Database brings model-specific settings and material-processing references into one place, helping you focus testing on your actual equipment and application.
- Find your combination: search by printer model and select the corresponding resin.
- Review the full entry: check the listed printing values rather than using exposure time alone.
- Match processing instructions: use the cleaning and curing conditions for the exact material.
- Confirm missing information: request help when your model is unlisted or the resin name does not match your bottle.
A reference profile narrows the starting point; it does not eliminate local testing. Keep a record of the profile you use and the adjustments confirmed on your machine.
Frequently asked questions
Can I use the same dental resin settings on Phrozen and Anycubic printers?
Do not assume the values transfer. Select the profile for the exact machine and material. Even printers from the same brand can require different exposure and motion settings.
What is the difference between normal exposure and bottom exposure?
Normal exposure applies to the regular printed layers. Bottom exposure applies to the initial layers used to establish adhesion to the build plate. Check the corresponding layer count and transition settings in the full profile.
Should I change exposure when changing layer height?
Use a profile for the new layer height or request guidance. Changing layer thickness changes the printing conditions, so the original exposure should not be assumed suitable.
How much should I increase or decrease exposure?
Use small, documented changes within the supplier's recommended range. There is no universal increment for every printer and resin. Change one variable at a time and compare the same test geometry.
Is one successful test print enough?
It is a useful first check. Confirm repeatability and evaluate representative parts after the required post-processing before accepting the settings for production.
Do printing parameters also confirm suitability for patient-contact applications?
No. Printing settings do not establish intended use or biological safety. For patient-contact parts, confirm the material documentation and complete prescribed workflow separately.
What if my printer or resin is not listed?
Send the full printer model, firmware and slicer versions, resin code and intended application to RayForm. Use the Support Center for current technical documents rather than substituting a similar-looking profile.
Sources & technical references
- RayForm — Dental Resin Printing Parameters & Post-ProcessingAll eight profile rows and the need to match printer, material and layer height. Checked September 23, 2026.
- RayForm — Water Washable Dental Model Resin (RF-ZJ-02)Different Sonic Mini 8K S reference values in product-specific documentation; resin-code confirmation is required. Checked September 23, 2026.
- Phrozen Help Center — How to Dial in Resin for Optimal ResultsXP Finder and visual assessment of exposure tests; no universal percentage increase is imported into this guide. Checked September 23, 2026.
- Anycubic — 3D Printer Test Print: Resin Exposure Range FinderExposure calibration and model-appropriate exposure test files. Checked September 23, 2026.
- Phrozen — Resin 3D Printing Troubleshooting GuideGeneral checks for plate adhesion, delamination, surface defects and support failure. Checked September 23, 2026.